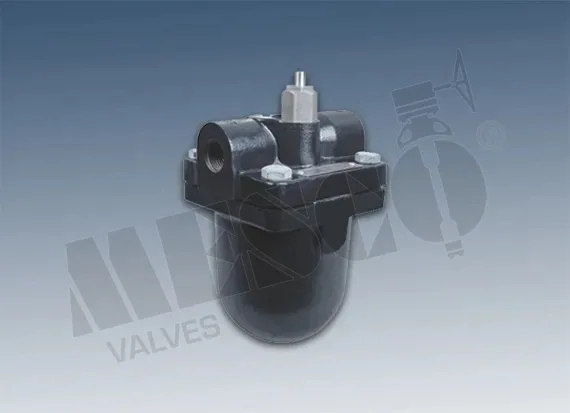
Steam Trap Valve
A Steam Trap Valve automatically removes condensate, air, and non-condensable gases from steam systems without allowing live steam to escape during normal operation, supporting heat transfer efficiency and helping prevent issues such as water hammer. Shree Ganesh Engineering Works, under the MESCO brand, provides steam trap valves for industrial applications, including steam pipelines, boilers, and heat exchangers. Selecting a suitable valve depends on Operating pressure, temperature, and condensate load to meet the system’s requirements.
Key Features of Steam Trap Valves
Automatic Condensate Removal
Discharge of the accumulated condensate from the steam system without any manual intervention.
Steam Conservation
This will help to minimize any wastage of live steam if chosen wisely.
Air Discharge
Assists in discharging air and non-condensable from suitable steam systems.
Heat Transfer Support
The discharge of condensate is helpful in ensuring efficient heat transfer from the steam system.
Equipment Protection
Helps in reducing the problem of water hammering and other associated issues with condensate build-up.
Application-Based Selection
It all depends on pressure, temperature, condensate load, etc.
Applications of Steam Trap Valves
The steam trap valve finds application in industries requiring steam for various purposes such as heating or processing. The applications include

Boiler Systems
To separate condensate from appropriate steam lines and associated apparatus.
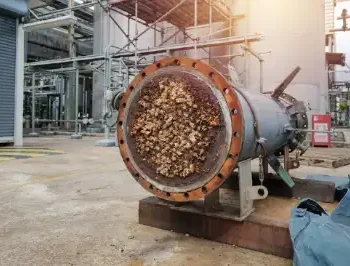
Heat Exchangers
Assists in discharging condensate for effective heat exchange.
Steam Distribution Pipelines
Separates the accumulated condensate from steam distribution system.
Food Processing Plants
Application in appropriate steam heating and processing systems.
Textile Industry
To assist in the steam supply systems employed in textile manufacturing.
Pharmaceutical Manufacturing
Application in appropriate steam systems based on processes.
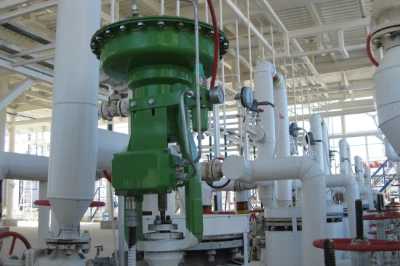
Chemical Plants
Appropriate in steam heating and processing equipment
Choose a Suitable Steam Trap Valve for Your System
The selection of the proper steam trap valve is essential for managing condensate as well as ensuring the efficiency of steam equipment in industries. Shree Ganesh Engineering Works under the name of MESCO provides various valve products based on industrial needs.
Our experts will guide you to choose the right valve for your specific application. Some of the parameters that should be taken into account during the selection process include steam trap pressure, temperature, load, etc.
Frequently Asked Questions
What is a steam trap valve used for?
A steam trap valve functions by automatically removing condensate, air, and other gases that are not condensable from the steam system without releasing any live steam.
How does a steam trap valve work?
A steam trap valve functions based on its design to remove condensate and other gases from the system and keep live steam in it.
Why is condensate removal important in steam systems?
The removal of condensate ensures that heat transfer is efficient and water hammer problems are avoided
Where are steam trap valves commonly used?
They are used in boilers, heat exchangers, steam lines, food processing factories, textile industries, chemical factories, and pharmaceutical manufacturing.
How do I choose the right steam trap valve?
It depends on pressure and temperature, condensate flow, steam conditions, equipment type, and discharge capacity
